JH-05PL Hot-Wire TIG Valve Cladding Machine
Precision Automated Cladding for Valve Bores, Seats and Complex Internal Geometries
The JH-05PL Valve Cladding Machine is a flexible automated welding system developed for precision overlay welding of valve bodies, internal bores, seat pockets and other complex internal surfaces.
The machine uses a Hot-Wire TIG cladding process combined with servo-controlled positioning, constant surface speed control, AVC arc voltage control, closed-loop motion control and programmable welding paths.
Compared with conventional manual TIG overlay welding, the JH-05PL provides more consistent control over torch position, arc length, welding speed, wire feed rate, welding current, welding voltage, workpiece rotation, surface travel speed, layer position and weld bead overlap.
The standard system is designed for internal diameters of approximately 70–350 mm and workpieces weighing up to 1000 kg.
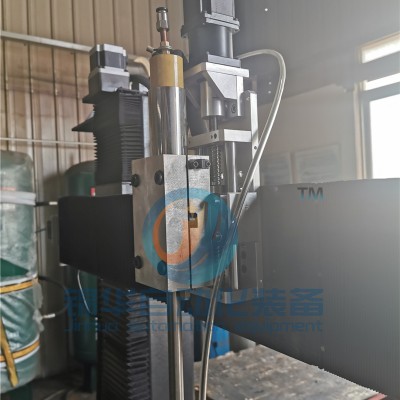
Key Capabilities
Standard capabilities of the JH-05PL valve cladding system, covering the working range, motion control, programming and data functions.
What Is the JH-05PL Valve Cladding Machine?
The JH-05PL is an automated TIG overlay welding system designed to deposit corrosion-resistant or wear-resistant alloy onto selected surfaces of a valve body.
Instead of manufacturing the entire component from an expensive corrosion-resistant alloy, the valve body can be manufactured from a structural base material and the critical sealing or process-contact surfaces can then be clad with the required alloy.
Typical cladding areas include:
- Internal valve bores
- Valve seats
- Seat pockets
- Branch bores
- Intersecting bores
- Ring grooves
- Internal cylindrical surfaces
- Tee intersections
- Complex valve cavities
This approach can provide the required surface performance while reducing the amount of high-alloy material used in the complete component.

Valve body cladding — critical internal surfaces clad with corrosion- or wear-resistant alloy.
Hot-Wire TIG Cladding Process
The JH-05PL uses a Hot-Wire TIG process. In this process, the welding wire is electrically preheated before entering the weld pool.
Compared with conventional cold-wire TIG welding, hot-wire technology can increase deposition efficiency while maintaining the stable and controlled characteristics associated with TIG welding.
The process is particularly suitable for applications requiring:
- Controlled dilution
- Consistent overlay thickness
- Smooth weld bead formation
- High-quality metallurgical bonding
- Accurate cladding of internal surfaces
- Controlled alloy deposition
Final welding parameters depend on the base material, filler wire, overlay alloy and required welding procedure.

Hot-Wire TIG cladding — electrically preheated filler wire entering the weld pool.
Constant Surface Speed & AVC Arc Voltage Control
Two control systems work together to keep the welding speed and the arc length consistent while the torch moves around internal valve geometry.
Constant Surface Speed Control
Valve components often contain surfaces with different diameters. If the workpiece rotates at a fixed RPM, the actual welding speed at the surface changes as the diameter changes.
The JH-05PL therefore supports Constant Surface Speed control.
The control system automatically adjusts workpiece rotation according to the actual welding diameter so that the torch maintains a more consistent linear welding speed.
This helps improve:
- Weld bead consistency
- Heat input control
- Overlay thickness
- Bead overlap
- Surface quality
AVC – Automatic Arc Voltage Control
Maintain a Stable Torch-to-Workpiece Distance
During automatic TIG cladding, changes in component geometry can cause the distance between the tungsten electrode and workpiece to vary.
The JH-05PL uses AVC – Arc Voltage Control to automatically compensate for these changes.
The system monitors arc voltage and adjusts the torch position to help maintain a consistent arc length.
Stable arc length contributes to:
- More stable welding
- Consistent penetration
- More uniform bead geometry
- Better surface quality
- Reduced operator intervention

Surface speed and arc length — rotation speed and torch position adjusted automatically.
Servo Control & Torch Positioning
Servo-controlled motion axes with closed-loop feedback position the welding torch precisely inside limited internal working spaces.
Full Closed-Loop Servo Control
The JH-05PL uses servo-controlled motion axes combined with feedback control. The closed-loop system continuously compares the commanded position with the actual machine position and makes corrections where required.
This improves control of:
- Torch positioning
- Welding trajectory
- Axis movement
- Workpiece location
- Repeat welding cycles
Precision motion control is especially important when cladding internal valve surfaces where available working space can be limited.
Servo-Controlled Torch Positioning
The welding torch is positioned through servo-controlled movement. The standard machine includes:
- X Axis — servo-controlled movement with approximately 32 in. travel
- Z Axis — servo-controlled vertical movement with approximately 40 in. travel
The large motion range provides flexibility for different valve body heights and internal welding locations.
Final axis travel should be confirmed according to the selected machine configuration.
Automatic Welding Program Generation
The JH-05PL is designed to simplify programming for common valve geometries. Operators can define key reference positions rather than manually creating every individual welding coordinate.
Built-In Valve Geometry Programs
The control system supports different programming methods for typical component structures.
Cylindrical Bore – Two-Point Programming
For simple cylindrical internal surfaces, the operator defines the required reference positions and the system generates the welding path.
Tee Connection – Four-Point Programming
Suitable for internal cladding around intersecting T-shaped valve passages.
The system uses programmed reference points to calculate the required welding trajectory around the intersection.
X-Joint – Four-Point Programming
Designed for complex internal crossings with four connecting passages.
Upper Branch Bore – Three-Point Programming
Allows automated cladding around upper intersecting ports or secondary bores.
Lower Branch Bore / Seat Pocket – Three-Point Programming
Designed for lower internal cavities and valve seat-pocket geometries.
Intersecting Cylindrical Bores
The JH-05PL can perform programmed welding around intersections between cylindrical holes.
This is particularly useful for valve bodies with multiple internal flow passages.
Ring Groove Programming
Dedicated ring-groove programming allows the system to clad circular groove surfaces automatically.
For simple cylindrical internal surfaces, the operator defines the required reference positions and the system generates the welding path.

Valve geometry programming — bore, tee, branch and ring-groove programs generated from reference points.
Wire Feeding & Specialized Internal Cladding Torches
Stable hot-wire feeding and geometry-matched torches determine whether internal valve surfaces can be clad accurately.
High-Precision Hot-Wire Feeding
The machine uses a controlled wire feeding system for the Hot-Wire TIG process. Stable wire delivery is critical because variations in wire feed directly affect:
- Deposition rate
- Overlay thickness
- Welding current balance
- Bead formation
The system coordinates wire feeding with workpiece movement and welding parameters.
Specialized Internal Cladding Torches
The JH-05PL can be configured with different TIG cladding torches according to the valve geometry. Available torch concepts can include:
- Small-bore torch
- Oval-profile torch
- Adjustable-head torch
- Long-reach internal bore torch
- Specialized seat-pocket torch
The correct torch is selected according to internal diameter, bore depth, valve geometry, welding position and required overlay area.
Compact Machine Design & Fast Setup
The compact mechanical layout provides substantial internal cladding capability while minimizing workshop footprint and setup time.
Compact Machine Design
One of the main advantages of the JH-05PL is its compact mechanical layout. The machine is designed to provide substantial internal cladding capability while minimizing workshop footprint.
This makes it suitable for:
- Valve production workshops
- Specialized weld overlay departments
- Repair facilities
- High-alloy component manufacturing cells
Fast Setup
The graphical HMI, servo positioning and built-in geometry programs are designed to reduce machine setup time.
For repeat valve specifications, stored welding programs can be recalled instead of recreating the complete process each time.
This helps reduce non-welding time between production cycles.
Remote Diagnostics & Monitoring
The control architecture can be configured for network connectivity. Depending on the final machine configuration and customer’s network permissions, remote connectivity can support functions such as:
- Diagnostics
- Machine status monitoring
- Technical troubleshooting
- Maintenance support
- Parameter review
Remote access should be implemented according to the customer’s cybersecurity and factory network requirements.
Typical Valve Cladding Applications
The JH-05PL can be applied to automated cladding of:
Actual workpiece compatibility depends on the internal geometry and available torch access.
Typical Overlay Applications
Depending on the customer’s welding procedure, the system can be configured for corrosion-resistant or wear-resistant overlays used in industries such as:
The final filler material is selected according to the service environment and required corrosion or wear resistance.
Typical Production Process
A ten-stage production sequence, from loading the valve body through to reviewing the recorded welding data.
Load the Valve Body
Place the workpiece onto the clamping / rotating system.
Select the Welding Program
Choose the appropriate geometry program according to the valve structure.
Define Reference Points
Teach the required bore, seat or intersection positions.
Set Welding Parameters
Enter the welding parameters before starting the cycle.
- Welding current
- Welding voltage
- Hot-wire parameters
- Wire feed speed
- Surface speed
- Weld overlap
Calibration
Perform the required machine and torch calibration.
Start Automatic Cladding
The servo system automatically controls the torch and workpiece according to the programmed path.
AVC Compensation
Arc Voltage Control continuously adjusts the torch position to help maintain a stable arc length.
Real-Time Monitoring
Actual welding parameters and machine positions are displayed on the HMI.
Complete the Overlay
The system automatically completes the programmed welding area.
Review Welding Data
Process data can be reviewed or stored for production and quality records.
Technical Specifications
Standard configuration data for the JH-05PL automatic hot-wire TIG valve cladding machine.
| Parameter | Specification |
|---|---|
| Model | JH-05PL |
| Machine Type | Automatic Hot-Wire TIG Valve Cladding Machine |
| Welding Process | Hot-Wire TIG |
| Internal Diameter Range | Ø70–350 mm |
| Maximum Workpiece Load | 1000 kg |
| Maximum Workpiece Height | 1000 mm |
| Main Control | PLC + HMI |
| X Axis | Servo Control, approx. 32 in. travel |
| Z Axis | Servo Control, approx. 40 in. travel |
| Wire Feeder | DC Drive |
| Constant Surface Speed | Yes |
| AVC Arc Voltage Control | Yes |
| Full Closed-Loop Control | Yes |
| Semi-Automatic Calibration | Yes |
| Metric / Imperial Switching | Yes |
| Real-Time Data Feedback | Yes |
| Welding Data Logging | Yes |
| Multi-Language Interface | Available |
| Program Capacity | Up to approximately 8000 program steps* |
| Internal Bore Programming | Yes |
| Tee Programming | Yes |
| X-Joint Programming | Yes |
| Branch Bore Programming | Yes |
| Intersecting Bore Programming | Yes |
| Ring Groove Programming | Yes |
| Remote Diagnostics | Optional / Network Configurable |
*Final program-memory specification should be confirmed according to the supplied control-system version.
Programming & geometry coverage
- Internal bore, tee, X-joint and branch bore programs
- Intersecting bore and ring groove programming
- Real-time monitoring of voltage, current and position
- Automatic height compensation and wire length counter

Programming Functions
Geometry programs and monitoring functions supported by the JH-05PL control system.
| Function | Supported |
|---|---|
| Simple Cylindrical Bore – 2 Point | Yes |
| Tee Connection – 4 Point | Yes |
| X-Joint – 4 Point | Yes |
| Upper Branch Bore – 3 Point | Yes |
| Lower Branch / Seat Pocket – 3 Point | Yes |
| Intersecting Cylindrical Bore | Yes |
| Ring Groove | Yes |
| Real-Time Voltage Monitoring | Yes |
| Real-Time Current Monitoring | Yes |
| Hot-Wire Voltage Monitoring | Yes |
| Wire Feed Speed Monitoring | Yes |
| Worktable Speed Monitoring | Yes |
| Real-Time Welding Position | Yes |
| Automatic Height Compensation | Yes |
| Wire Length Counter | Yes |
Operating Environment
Ambient and supply requirements for installing the JH-05PL in a valve production or overlay workshop.
| Requirement | Specification |
|---|---|
| Ambient Temperature | -10°C to +40°C |
| Relative Humidity | ≤95%, non-condensing |
| Working Environment | Well ventilated, without severe mechanical impact |
| Power Frequency | 50 Hz |
| Standard Electrical Supply | To be confirmed according to final machine configuration |
| Export Voltage | Customizable according to destination country |
Why Choose the JH-05PL?
Eight practical reasons why the JH-05PL suits valve manufacturers and overlay departments working with complex internal geometry.
Designed for Complex Valve Geometry
The machine is not limited to simple cylindrical bore welding. It supports multiple internal geometries including:
- Seat pockets
- Branch bores
- T intersections
- X intersections
- Ring grooves
Hot-Wire TIG Process
Provides a balance between controlled TIG welding quality and improved deposition efficiency.
Constant Surface Speed
Automatically compensates for different welding diameters.
AVC Arc Length Control
Helps maintain stable torch-to-workpiece distance during automatic welding.
Closed-Loop Servo Motion
Improves positioning and repeatability for internal valve cladding.
Data Logging
Provides process information for quality control and production traceability.
Fast Programming
Built-in geometry functions reduce manual programming requirements.
Remote Support Capability
Network connectivity can be configured for diagnostics and maintenance support.
Send Us Your Valve Drawing
For a technical proposal, please provide:
- 01 Valve type
- 02 Valve body drawing
- 03 Internal bore diameter
- 04 Bore depth
- 05 Workpiece height
- 06 Workpiece weight
- 07 Base material
- 08 Required cladding alloy
- 09 Required overlay thickness
- 10 Required welding area
- 11 Valve seat / branch geometry
- 12 Welding procedure requirements
- 13 Factory power supply
- 14 Destination country
JINHUA engineers will evaluate the valve geometry and recommend the appropriate machine, welding torch and Hot-Wire TIG cladding configuration.
Request a Technical Proposal
Complete the form and JINHUA engineers will evaluate the valve geometry and recommend the appropriate machine, welding torch and Hot-Wire TIG cladding configuration.
Frequently Asked Questions
Common questions about the JH-05PL working range, Hot-Wire TIG process and control functions.
The JH-05PL is designed for automated Hot-Wire TIG overlay welding of valve internal bores, seats, pockets, branch connections and other complex internal surfaces.
The standard specified working range is approximately Ø70–350 mm.
Final accessibility depends on bore depth, valve geometry and selected welding torch.
Hot-Wire TIG uses electrically preheated filler wire during TIG welding.
The process can improve deposition efficiency while maintaining controlled TIG overlay quality.
AVC stands for Arc Voltage Control.
The system adjusts the torch position according to arc voltage feedback to help maintain a consistent arc length.
The machine automatically adjusts rotation speed according to the welding diameter so the actual linear welding speed at the surface remains more consistent.
Yes. The system supports programming functions for internal seat-pocket and branch-bore geometries.
Yes. The control system supports integrated process data recording and real-time feedback.
Yes. The HMI allows real-time switching between metric and imperial measurement systems.
Yes, depending on the final control and factory network configuration.
Remote diagnostics and monitoring functions can be integrated according to customer cybersecurity requirements.